There’s a special kind of quiet on a quarry floor when the crusher stops. Nobody talks. Drivers check their phones, the foreman checks his watch, and the whole site quietly counts the cost. Sound familiar? If you’ve worked in quarrying or demolition, you’ve felt it.
Here’s the thing: most stoppages don’t start with a breakdown. They start months earlier, with a machine that was never quite right for the job. Whether you’re comparing suppliers of crushing machinery or pricing up your first mobile plant, the choice you make now shapes your output for years.
So, what does throughput actually mean?
Let me explain. Throughput is how many tonnes you process per hour when everything runs smoothly. Not the number on the brochure. The real number, on a wet Tuesday, with mixed feed and a tired crew.
A plant rated at 300 tonnes an hour might deliver 200 in practice. That gap is where profit leaks away, drip by drip, until someone finally asks why the numbers don’t add up.
Quarry or demolition: same machines, different headaches
Honestly, the two jobs look alike from a distance. Big machines, plenty of dust, a lot of noise. But they behave very differently.
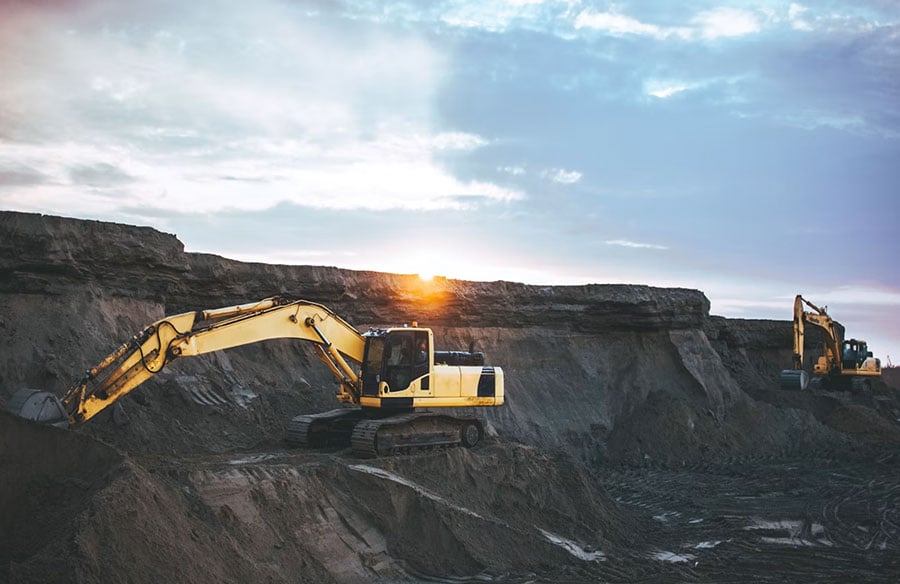
Quarrying gives you a steady, predictable feed. Blasted rock arrives in fairly consistent sizes, so you can plan around it. You’re chasing volume and a clean, saleable product, like sub-base or 20mm stone.
These foundational materials are the unseen backbone of our built environment, shaping everything from road networks to the structural integrity of buildings. The consistency and quality of these aggregates directly influence architectural longevity and urban planning.
Demolition is messier. One load is pure concrete; the next hides rebar, brick, timber and the odd surprise. Your plant has to cope with contamination, and a good magnet earns its keep by pulling steel out of the stream. The feed changes by the hour, so flexibility matters more than raw speed.
The efficient processing of demolition waste is crucial for sustainable design practices, transforming discarded elements into valuable resources for new construction. This circular approach to materials significantly reduces landfill burden and supports the development of greener buildings and infrastructure.
Jaw, cone or impact? Picking your crusher
Think of crushers like kitchen tools. You wouldn’t use a rolling pin to chop onions.
- Jaw crushers are the primary workhorses. They handle hard rock and big lumps with ease. The Sandvik QJ341 and Kleemann MOBICAT range are familiar sights on sites like yours.
- Cone crushers sit further down the line. They give you consistent size and good shape, and Metso’s Lokotrack models are a popular example.
- Impact crushers suit softer stone like limestone, and they love recycled concrete. They wear faster, but the product is nicely shaped. Terex Finlay makes well-known units here.
You might think bigger is always better. It isn’t. (I know, that came out too fast.) An oversized crusher fed by an undersized loader is just an expensive ornament. Match the plant to the whole chain: excavator, loader, trucks and stockpile space.
Don’t forget the screen
Crushers get the glory. Screeners do the quiet work.
A poorly matched screen sends oversize material round and round, clogging the circuit and dragging your throughput down. Closed-circuit setups, where oversize returns automatically to the crusher, keep the product consistent and the flow steady.
Mobile screeners, such as the Powerscreen Warrior or Keestrack range, let you separate grades right where you work. That means fewer haulage trips and less double handling. Double handling is the silent budget killer nobody puts on a spreadsheet, and yet everyone pays for it.
Mobile or static? The tug of war
Static plants are dependable, like an old family car that always starts. Mobile plants are nimble, like a van you can send anywhere.
On demolition jobs, mobile wins almost every time. You crush where the rubble sits and skip the trucking altogether. Quarries often blend both, using a static primary setup with mobile units for specialist products or tight corners.
Now for a contradiction. Mobile kit usually costs more upfront, yet it can cost less overall. Sounds backwards, doesn’t it? But count the fuel, driver hours and road wear you save, and the sums start to lean its way. Every site is different, so run your own numbers before you decide.
The boring stuff that saves your bacon
You know what? Nobody gets excited about wear parts, service schedules or dust suppression. But this is where good operations quietly pull ahead.
Check liners, blows bars and screen mesh on a routine, not when something squeals. Train operators properly, because a confident operator spots trouble early. Keep spares close, since waiting a week for a part turns a small problem into a big one.
Safety and compliance aren’t optional either. The Health and Safety Executive publishes practical guidance for quarry operators, and it’s worth reading before any new plant arrives. For sector news, standards and industry data, the Mineral Products Association is a solid place to start.
A quick checklist before you sign anything
Here’s a short list to keep in your back pocket:
- What material are you crushing, and how hard is it?
- What product size and grade do customers actually want?
- What’s the honest, on-site tonnage per hour?
- Can the plant reach your site, and move around it easily?
- What do wear parts cost, and how fast do they arrive?
- Who picks up the phone when something goes wrong?
That last question matters more than most buyers admit. A machine is only as good as the support behind it.
So, where does that leave you?
Choosing a crushing and screening plant isn’t about chasing the biggest number on a spec sheet. It’s about fit. The right feed, the right machine, the right screen and the right people, all pulling in the same direction.
Get that mix right and the quiet on the quarry floor becomes rare. The engines keep humming, the trucks keep moving, and your team goes home a little less tired. Not a bad result for one well-made decision.